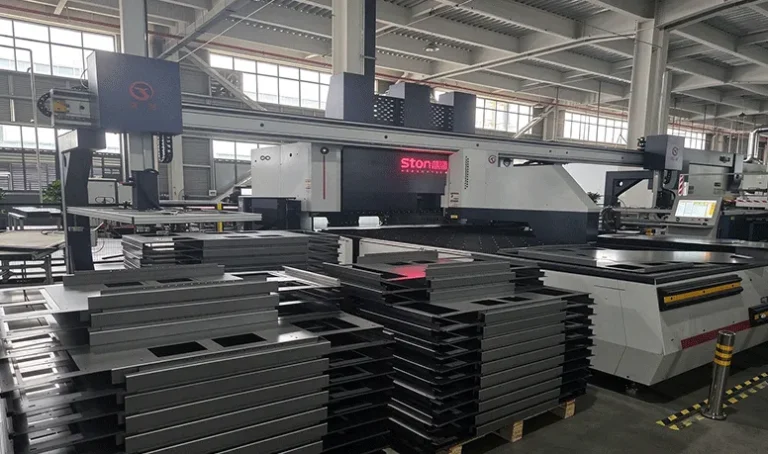
Sheet metal forming reshapes flat sheet into three-dimensional parts by plastic deformation, without removing material. The common methods are bending, punching with forming tools, and flanging. Results depend on material thickness, bend geometry and machine type: STON’s panel benders handle cold-rolled steel up to 2.0 mm, stainless up to 1.2 mm, and aluminium up to 2.5 mm.
What counts as forming, and what doesn’t
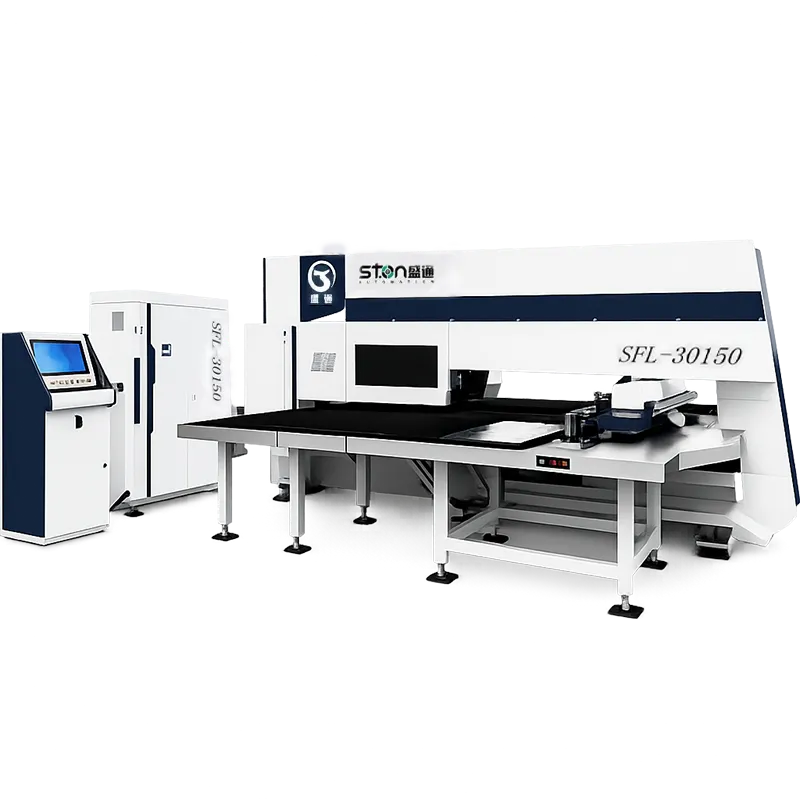
Forming changes the shape of a sheet and leaves its mass intact. Cutting (laser, shearing) and punching a through-hole remove material and belong to blanking. The two overlap in practice because a turret punch press does both: it punches holes and also forms louvers, embosses and ribs in the same cycle.
The reason the distinction matters to a buyer is that forming limits come from the material’s yield behaviour and the machine’s force and geometry, while cutting limits come from power and edge quality. A 2 mm sheet that a laser cuts easily may still be too thick for a given bender.
Four forming routes in a sheet metal shop
| Route |
Typical machine |
What it does |
Where it fits |
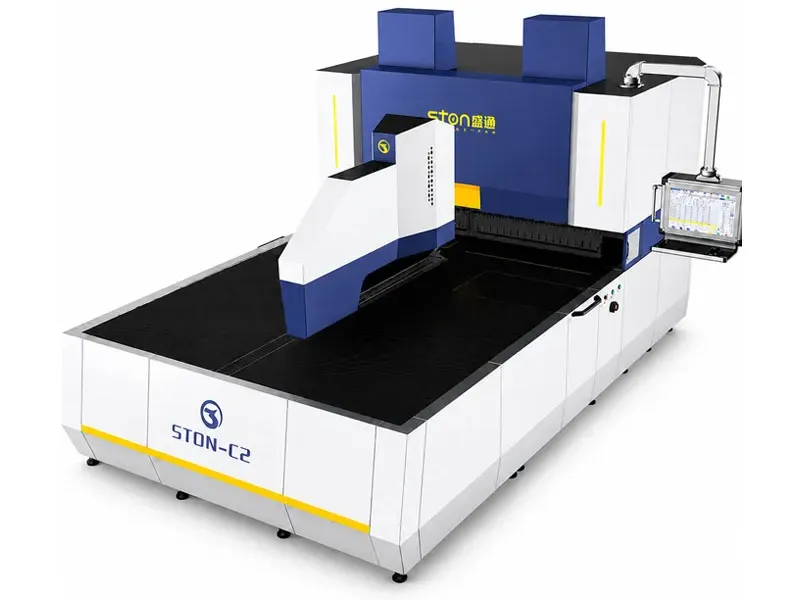
| Panel bending |
آلة ثني الألواح باستخدام CNC |
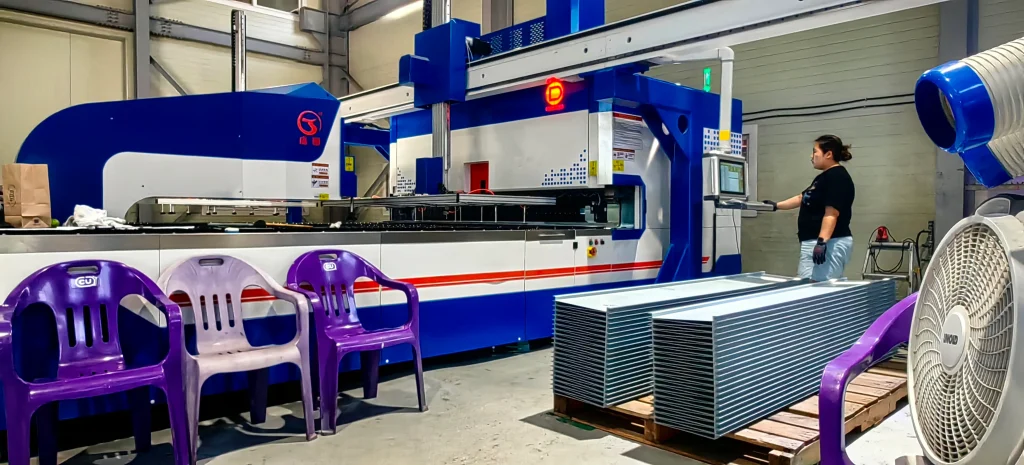
Holds the sheet and folds each edge in sequence, rotating the part rather than the operator |
Cabinet doors, drawers, ventilation panels |
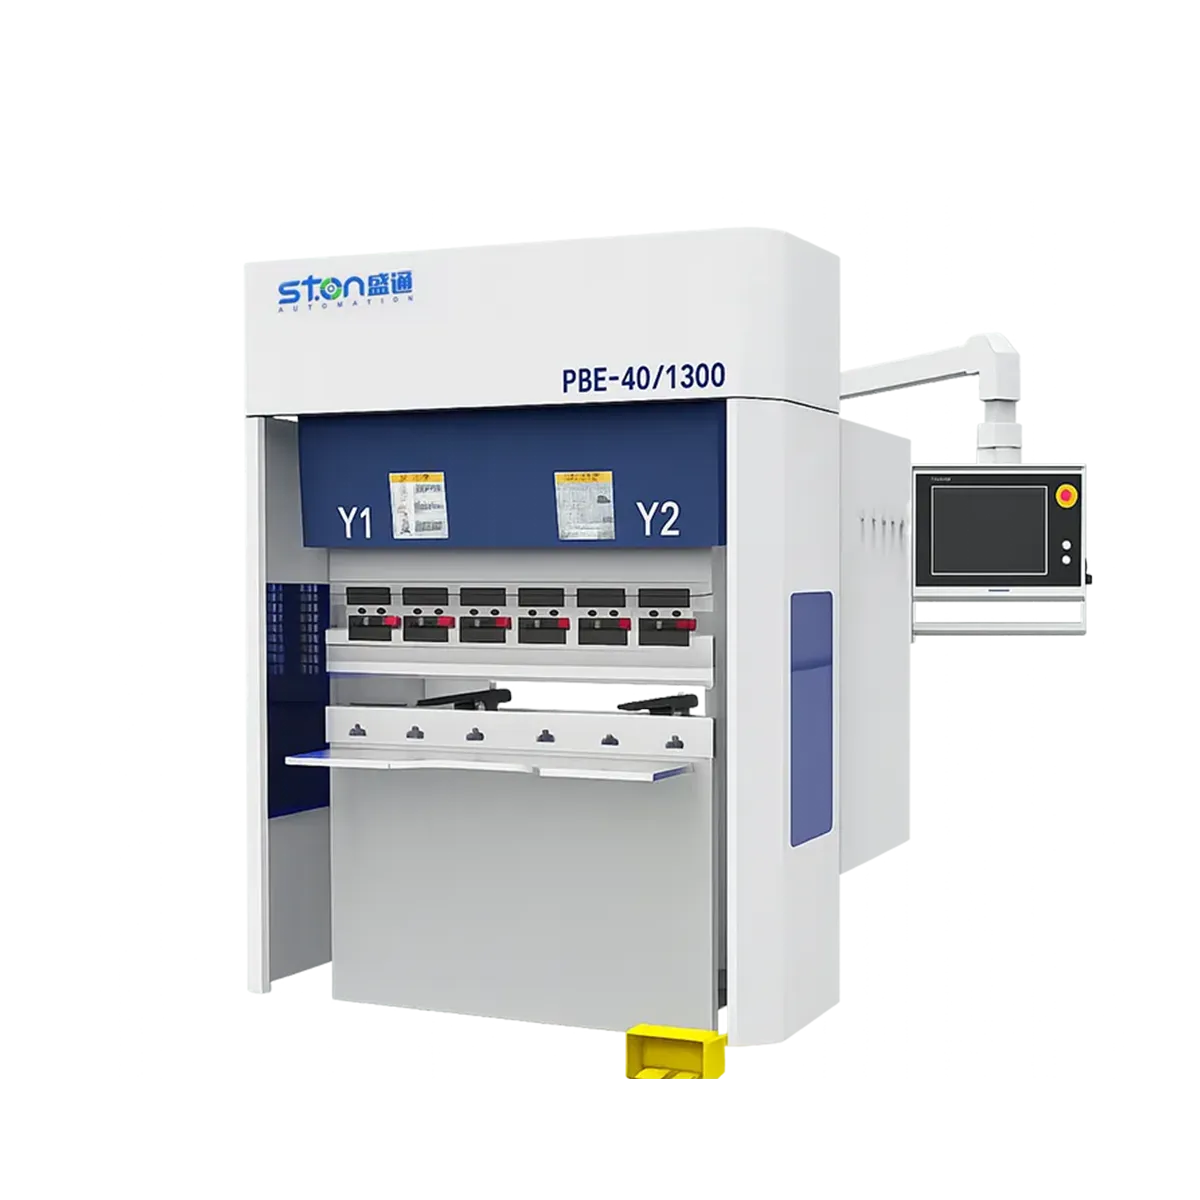
| Press brake bending |
Electro-hydraulic or pure-electric CNC press brake |
Bends along a line between punch and die |
General sheet metal, enclosures, appliance housings |
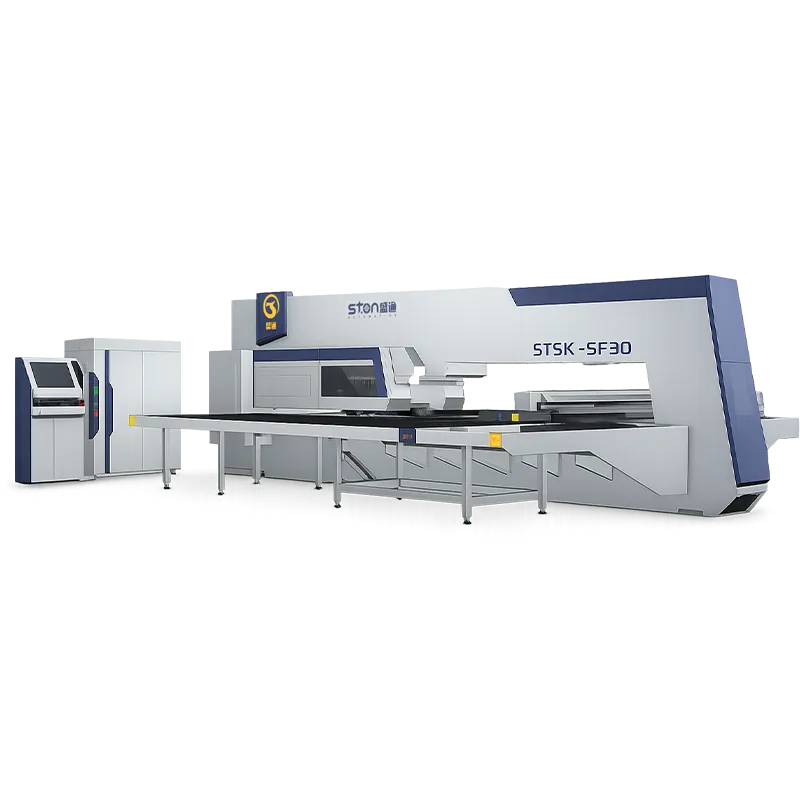
| Punch forming |
CNC turret punch press |
Punches, forms, embosses and louvers with a tool turret |
Perforated sheet, switchgear panels, ventilation plates |
| Flanging / folding |
Flexible edge bending (folding) machine |
Folds edges with a flip-plate beam; arc, dead-edge and offset processes are available |
Large flat panels with returned edgesg |
STON’s documentation lists all four. The choice between them is mostly about batch size, part variety and how many bends each part carries, which is why a bender-versus-brake decision belongs in a separate comparison.
Material and thickness: the limit that decides everything else
Thickness limits are published per material because stainless steel springs back harder and resists forming more than mild steel, while aluminium forms easily but marks and cracks along tight radii.
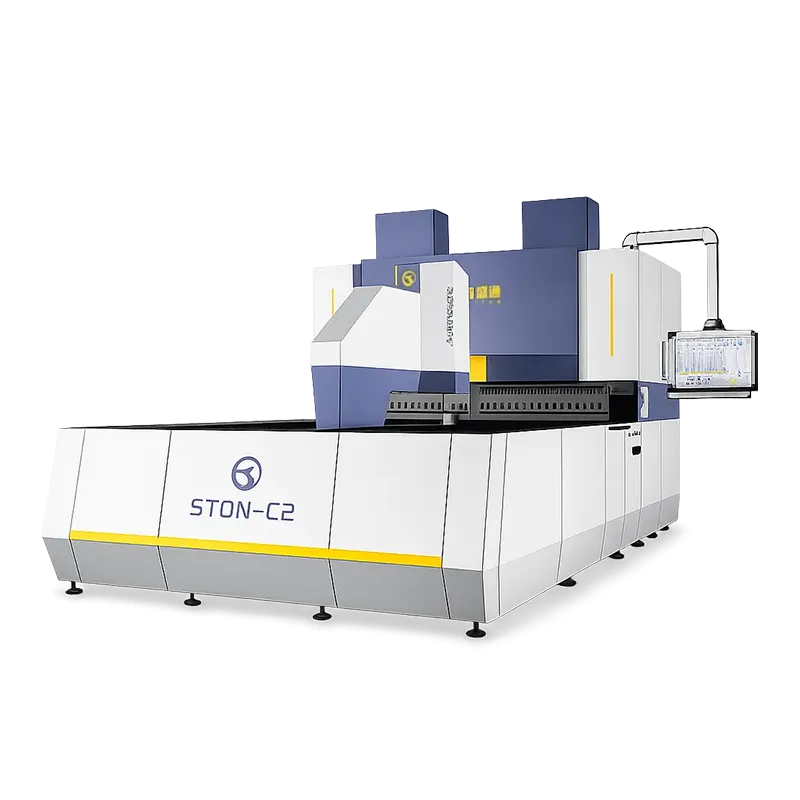
STON آلة ثني الألواح باستخدام CNC, Press Arm Type (spec sheet values, “maximum bending thickness at full bend”):
| Frame |
Max bending size (mm) |
Cold-rolled steel |
Stainless steel |
| A (1000), welded |
1000 × 1000 |
1.5 mm |
1.0 mm |
| B (1400), welded |
1400 × 1250 |
1.5 mm |
1.0 mm |
| B (1400), cast |
1400 × 1250 |
2.0 mm |
1.2 mm |
| C (2000), cast |
2000 × 1500 |
2.0 mm |
1.2 mm |
| D+ (2800), cast |
2800 × 1500 |
2.0 mm |
1.2 mm |
Two points in that table are easy to miss. First, the cast-frame variants carry 0.5 mm more steel capacity and 0.2 mm more stainless capacity than welded frames of the same size. Second, the column is labelled “at full bend”, so the figure refers to a bend running the full machine length. The same sheet folded over a short edge is a lighter job.
STON’s family summary also lists aluminium up to 2.5 mm and an overall working range of 0.15–2 mm. The 0.15 mm lower figure is a reminder that very thin foil-like stock is a handling problem more than a force problem.
A common mistake: treating one thickness number as valid for every material on a quote. A buyer who runs 1.5 mm cold-rolled steel and 1.5 mm stainless should check the stainless figure separately, because on the welded frames above it is 1.0 mm.
Machine parameters for CNC press brakes and panel benders
For readers sizing a machine, here is the parameter set from STON’s documentation.
Electro-hydraulic CNC press brake (spec sheet range):
| المعلمة |
Range across models 63/1500 to 320/4100 |
| وزن الماكينة |
4,500–19,000 kg |
| قدرة المحرك الرئيسي |
8.7–22 kW |
| حجم الزيت الهيدروليكي |
130–500 L |
| شوط الأسطوانة |
215–315 mm |
| Controller options |
DELEM 53T, 58T, 66T, 69T; ESA optional |
| Deflection compensation |
Mechanical compensation system |
| Position feedback |
Grating ruler, closed loop |
STON also lists a laser protection device that stops the machine when a person or object enters the guarded zone. For hydraulic press brakes sold into the EU, EN 12622 is the product safety standard to check, alongside the CE conformity process.
The spec sheet for the pure-electric press brake (PBE series) gives mechanical data but no maximum material thickness, and neither sheet publishes a bending-thickness limit per tonnage. If your part is thicker than 2 mm cold-rolled steel, ask STON for the tonnage-versus-thickness chart for the model you are considering; do not infer it from the machine weight.
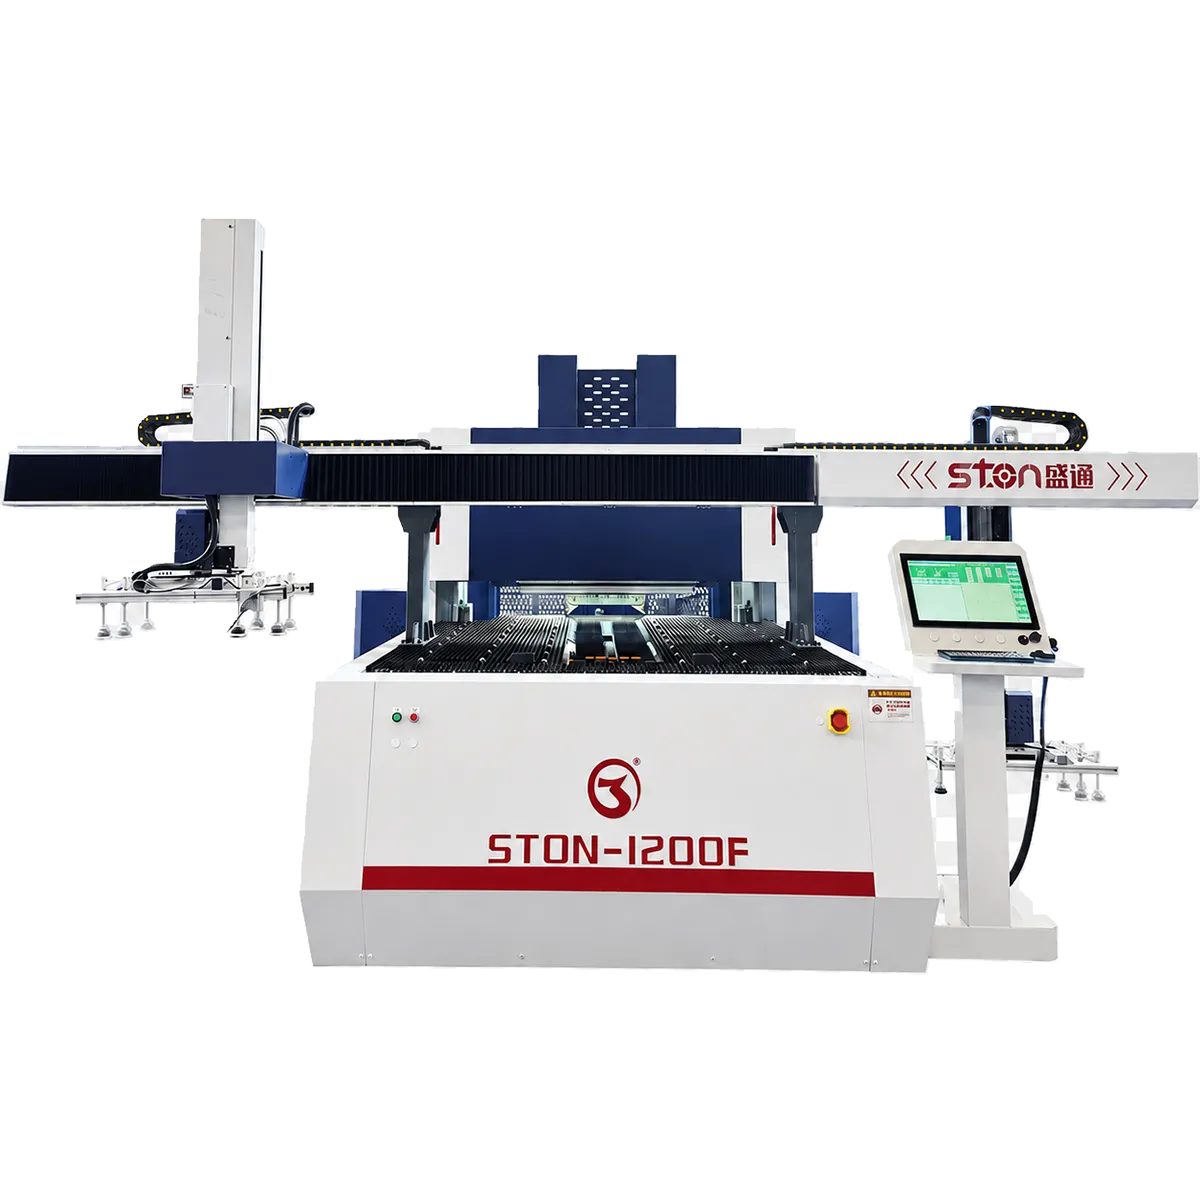
ماكينة ثني الألواح CNC, other published figures: servo axis count is 15 on the standard model, three-phase 380 V supply, 0.6 MPa compressed air, and a native loading/unloading interface for robot arms or gantries.
Five steps to test whether a part is formable on a given machine
- Write down material, grade and thickness for every part, and separate stainless from carbon steel.
- Compare each thickness with the per-material limit for the frame type you are considering (welded versus cast changes the number).
- Check geometry: bending height (minimum 5 mm on the Vacuum Type panel bender), minimum inner size for four-sided boxes, and the longest bend against the machine’s length.
- Decide which ISO 2768 class applies to unmarked dimensions, and mark every dimension that needs tighter control individually.
- Ask for a sample bend on your real material and measure it against your drawing. STON supports sample validation before shipment.
Compared with other approaches, and the honest limits
Compared with conventional press-brake workflows where an operator repositions the sheet for each bend, a panel bender handles the part rotation itself and keeps bend sequence in the program. That is a throughput and consistency argument for repeat parts with several bends per piece.
The limits are practical. A panel bender’s published thickness ceiling on welded frames is 1.5 mm for cold-rolled steel, so a job that is mostly 3 mm plate is a press brake job. Parts with very long flanges, or low batch counts with unusual geometry, may not recover the cost of a CNC panel bender. And no machine fixes a mismatch between the tolerance a drawing asks for and the tolerance the material can hold.
الأسئلة الشائعة
What is the difference between sheet metal forming and sheet metal fabrication?
Forming is one operation: shaping the sheet by plastic deformation. Fabrication is the whole chain: cutting, forming, joining and finishing.
What is the maximum stainless steel thickness a STON panel bender can fold?
1.0 mm on welded-frame models and 1.2 mm on cast-frame models in the Press Arm Type table, at full bend length.
Which ISO standard sets bending tolerances?
ISO 2768 sets general tolerances for dimensions without individual tolerances; it is not a bending-specific standard. Your drawing note decides which class applies.
Is ISO 286 relevant to bent parts?
Only where a formed or punched feature must fit another part as a hole-and-shaft pair. It does not govern flange lengths or bend angles.
Can one machine handle both thin and thick sheet?
Within a published range, yes. STON lists 0.15–2 mm overall for its panel benders. Outside that range, the answer is a different machine type, such as a press brake.
How should I verify a supplier’s accuracy claim?
Ask which number is machine positioning and which is part accuracy, then request a sample bend in your material. STON’s own sheets show how far apart two accuracy figures can be.


 19 أكتوبر 2026