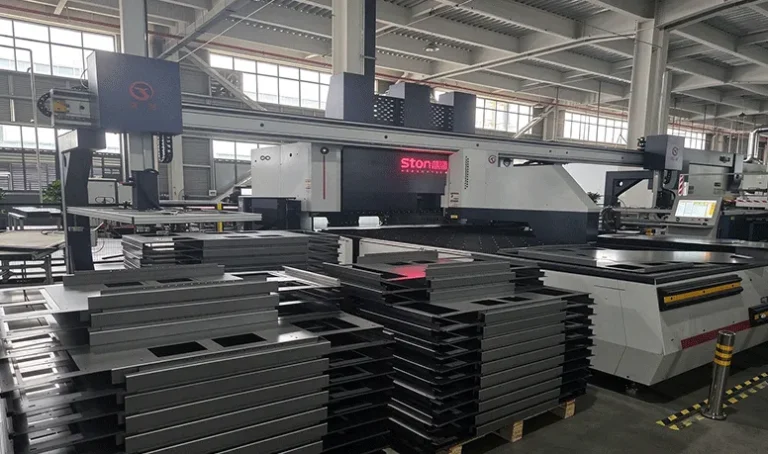
Choosing between a press arm and suction cup CNC panel bender is not simply about machine speed. A machine may support your material and bending dimensions but still struggle to position perforated, coated, or irregularly shaped panels.
The real question is: Which feeding system can handle your actual workpieces reliably throughout the complete bending process?
A press arm CNC panel bender uses mechanical positioning to control the sheet, while a suction cup panel bender uses vacuum-based handling. Press arm feeding is worth evaluating for suitable, repeatable panel geometries. Suction cup feeding provides an alternative when a customized vacuum contact arrangement better matches the workpiece. Neither is universally superior; the right choice depends on part drawings, contact areas, surface conditions, bending geometry, and production requirements.
This guide uses STON’s two panel bender configurations to explain their differences and provides a practical selection method for sheet metal manufacturers.
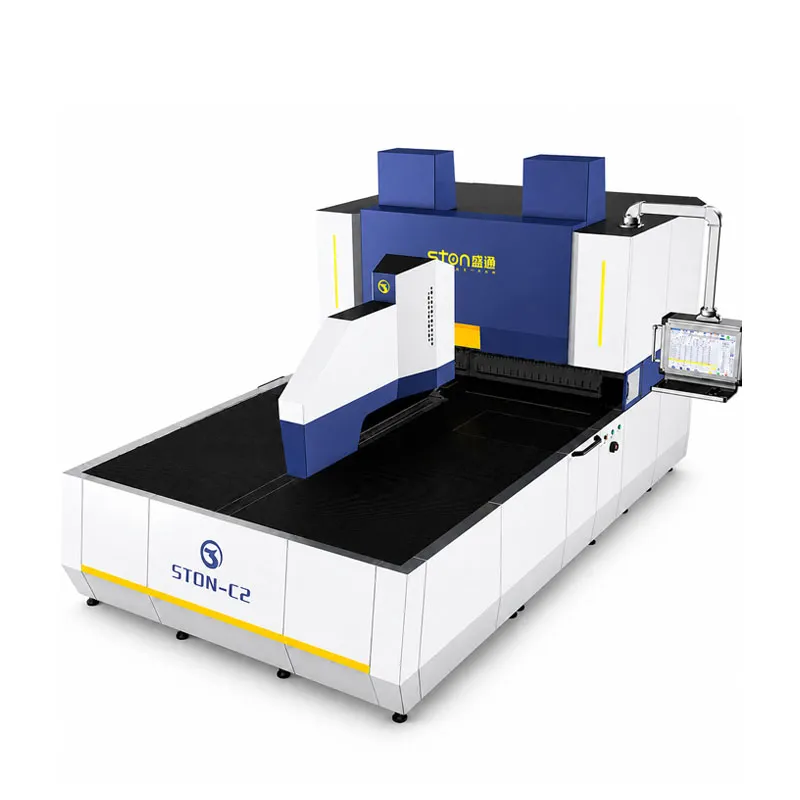
1. What Is the Difference Between Press Arm and Suction Cup CNC Panel Benders?
Both configurations automate sheet metal panel bending, but they use different methods to hold, position, and move the blank.
A press arm panel bender uses a mechanically controlled positioning arrangement. A suction cup panel bender uses vacuum suction assemblies to establish suitable contact with the sheet during handling.
This difference becomes important when a workpiece contains openings, irregular edges, a sensitive surface finish, or other features that affect its available contact areas.
Press Arm vs Suction Cup: Key Differences
| Comparison Factor |
Press Arm Panel Bender |
Suction Cup Panel Bender |
| Feeding method |
Mechanical press-arm positioning |
Vacuum suction-based feeding |
| Workpiece contact |
Mechanical holding areas |
Suitable suction contact areas |
| Main consideration |
Grip accessibility and movement clearance |
Vacuum sealing and holding reliability |
| Perforated sheets |
Check interference with holes and cutouts |
Confirm sufficient solid suction areas |
| Irregular profiles |
Evaluate mechanical gripping geometry |
Evaluate customized suction positions |
| Sensitive surfaces |
Verify contact pressure and potential marking |
Verify suction contact and surface condition |
| Production evaluation |
Complete mechanical positioning and bending test |
Complete suction handling and bending test |
The feeding system is only one part of machine selection. Material thickness, unfolded sheet dimensions, bending height, tooling, and the required forming sequence must also match the selected model.
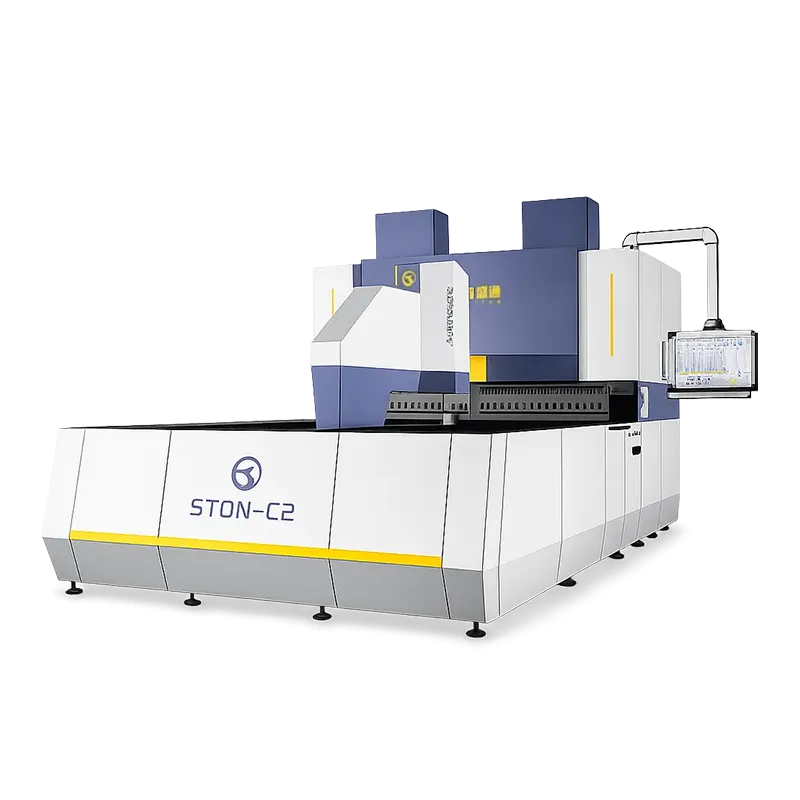
STON offers both configurations within its CNC Panel Bender product range.
2. When Should You Choose a Press Arm CNC Panel Bender?
A press arm CNC panel bender is worth considering when the workpiece provides suitable mechanical positioning areas and your factory needs repeatable, programmed bending.
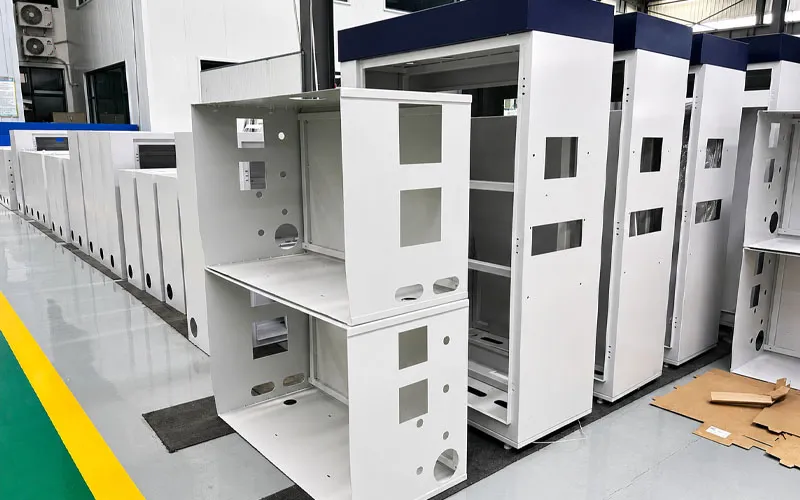
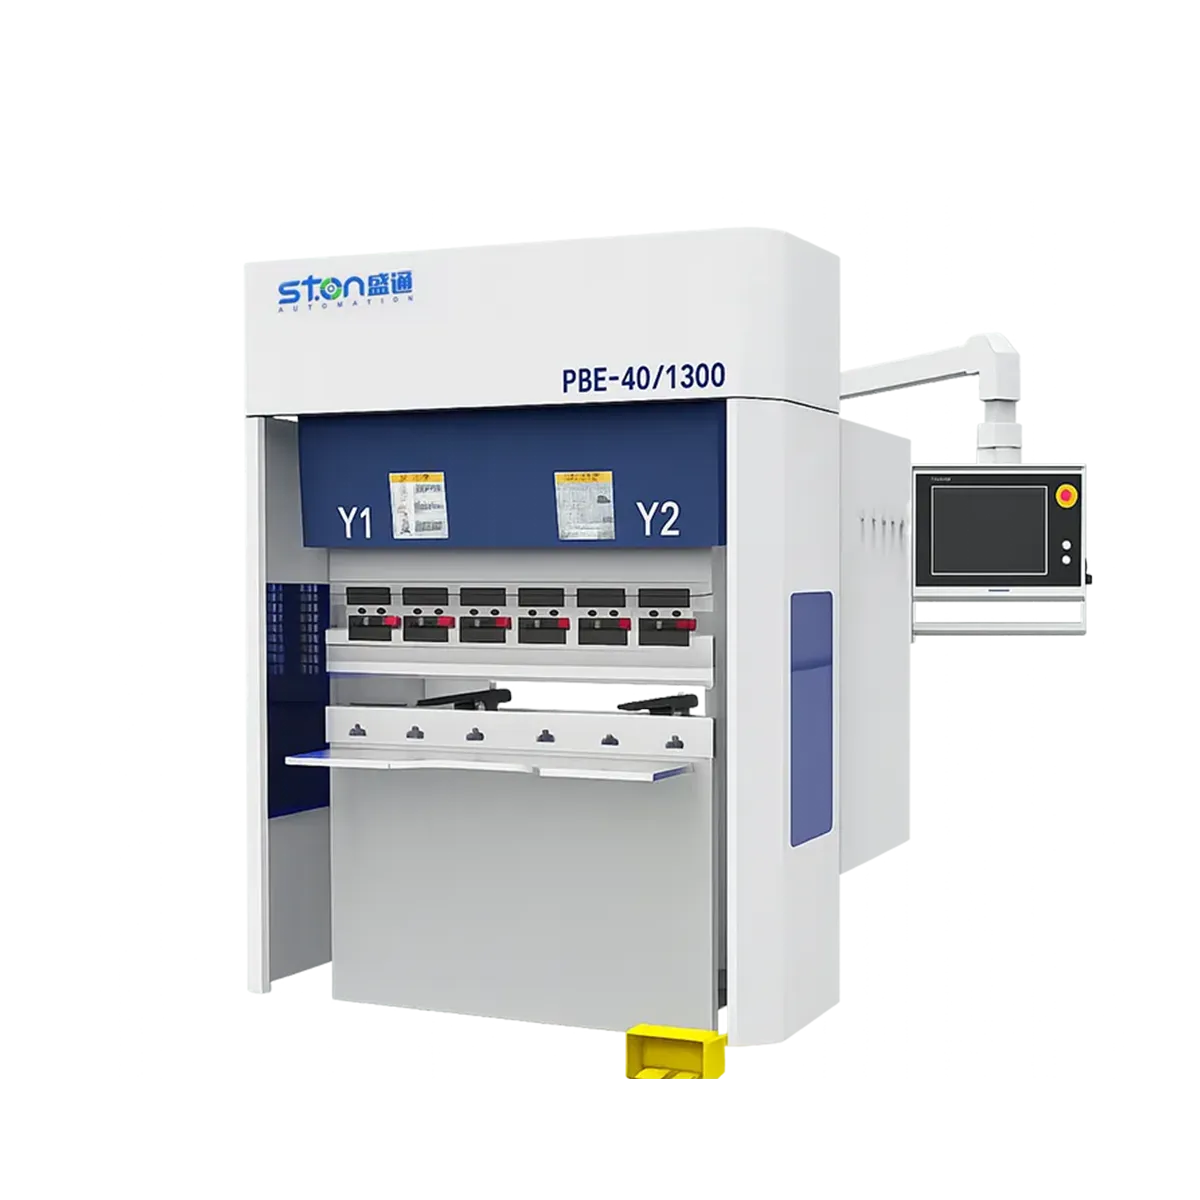
STON’s press arm range is designed for panel-type sheet metal products such as cabinets, enclosures, doors, frames, and metal furniture components. Its machine configurations combine CNC control, a rigid machine structure, servo-driven movement, and bending compensation features.
Where does press arm feeding offer value?
Repeatable cabinet production
A manufacturer processing recurring cabinet doors, drawer panels, or enclosure components can evaluate press arm feeding for stable, repeated positioning.
Mechanically controlled handling
The workpiece is positioned through a defined mechanical arrangement, which should be assessed against the actual drawing and bending program.
Production integration
STON’s press arm machines can be evaluated with compatible robotic, gantry, or truss loading arrangements when planning further automation.
What should you check before selecting it?
The main concern is whether the mechanical holding arrangement can access and move the part correctly.
A sheet with a large opening, narrow section, or special cutout may require closer evaluation. Operators should also confirm that the positioning components will not interfere with formed features or the subsequent bending sequence.
For visible surfaces, mechanical contact and the finished appearance should be checked using actual production material.
3. When Is a Suction Cup CNC Panel Bender More Suitable?
A suction cup CNC panel bender uses a vacuum-based assembly to hold and position suitable sheet metal blanks.
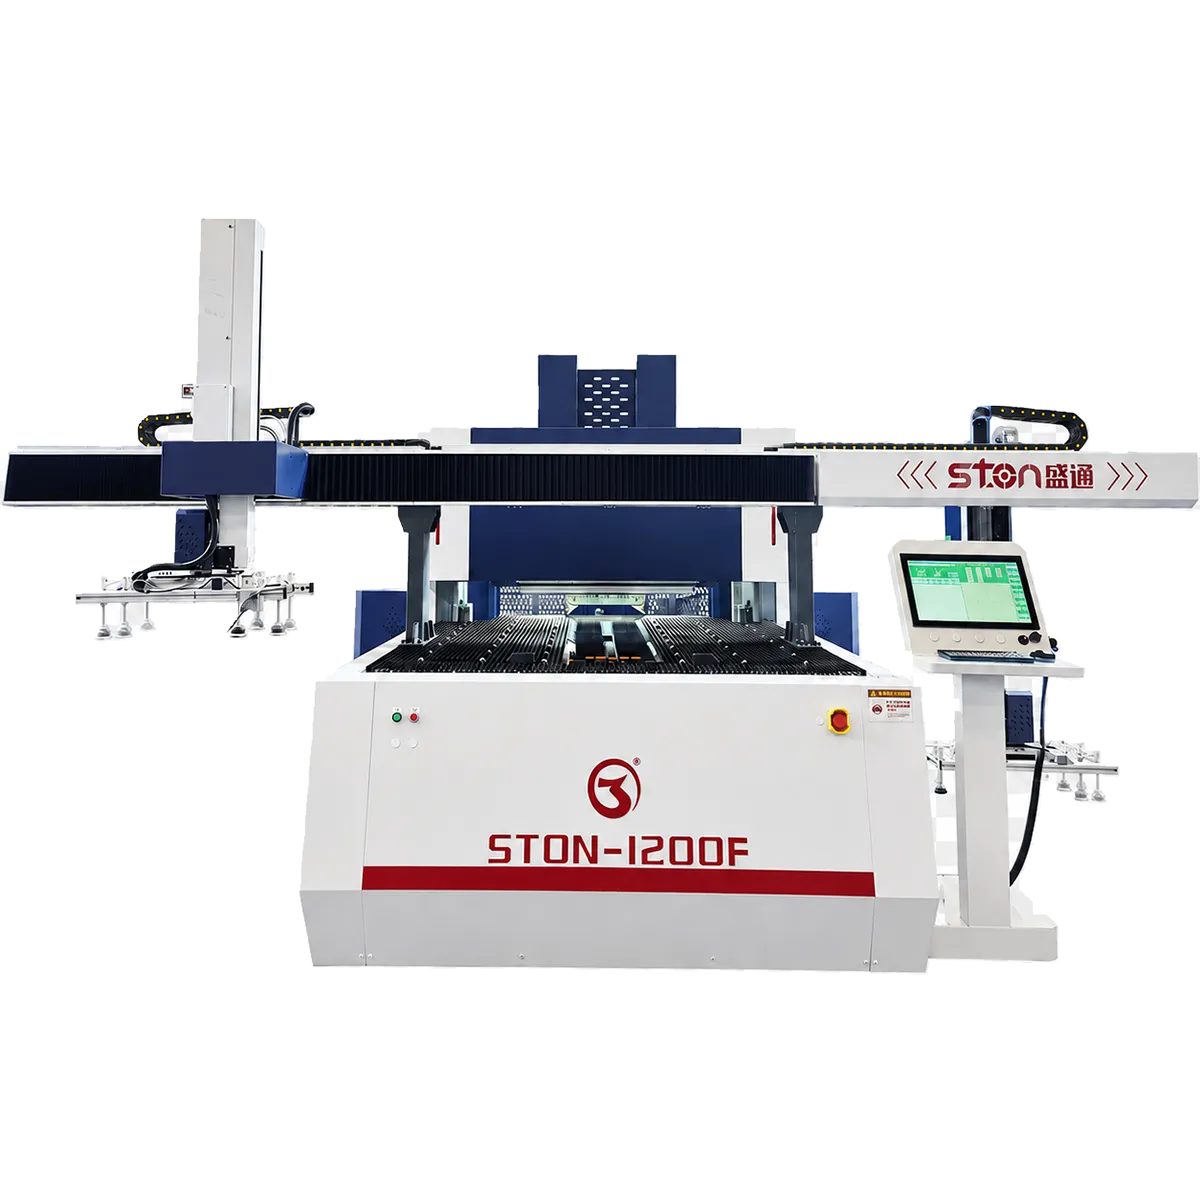
STON’s suction cup configuration combines customizable suction cup assemblies, all-electric servo closed-loop control, and coordinated multi-axis movement.
The ability to configure suction positions makes it an option worth examining when a different contact arrangement is needed for the workpiece.
However, vacuum handling must be verified against the actual material and blank structure.
What determines suction cup compatibility?
Available contact area
The blank must provide suitable areas where the suction cups can establish reliable contact.
Surface condition
Oil, dust, coatings, protective films, texture, and other surface characteristics can affect vacuum holding performance.
Blank shape and openings
Large openings or extensive perforations may limit suitable suction positions. A customized arrangement may be required.
Handling requirements
The suction system must support the workpiece’s dimensions, weight distribution, positioning movements, and bending sequence.
Does suction feeding guarantee better surface protection?
No. Although vacuum handling uses a different contact method from a mechanical press arm, that does not automatically make it scratch-free.
The condition of the suction cups, material surface, movement path, and contact locations can all affect the finished part.
If your products have visible stainless steel, coated, or decorative surfaces, request a handling and bending test using the actual production material.

4. How Do You Choose a Feeding System Based on Your Actual Parts?
The most practical selection method is to begin with the workpiece rather than the machine name.
A solid cabinet door, a perforated ventilation panel, and a decorative stainless steel cover may have different positioning requirements even when their overall dimensions are similar.
The following table identifies what should be evaluated before choosing either feeding system.
Workpiece-Based Panel Bender Selection Guide
| Workpiece Condition |
Press Arm: What to Check |
Suction Cup: What to Check |
| Standard rectangular panels |
Mechanical holding positions and movement |
Available suction area and positioning |
| Heavily perforated sheets |
Whether openings interfere with holding |
Whether sufficient solid suction areas remain |
| Large central cutouts |
Grip access and workpiece support |
Suction positions around the opening |
| Irregular external profiles |
Mechanical positioning clearance |
Feasibility of a customized suction layout |
| Decorative stainless steel |
Contact pressure and possible marks |
Vacuum contact, residue, and surface condition |
| Coated or pre-painted panels |
Holding contact and coating protection |
Suction cup and coating compatibility |
| Large cabinet panels |
Machine capacity and stable handling |
Machine capacity and holding reliability |
| Mixed production orders |
Compatibility across different part drawings |
Compatibility across different suction layouts |
Important: These are engineering evaluation criteria, not guaranteed processing capabilities. The final recommendation should be confirmed for the exact machine model and representative workpieces.
Example: A perforated electrical cabinet panel
Consider a hypothetical cabinet panel with ventilation holes, cable openings, and folded edges.
A press arm evaluation would examine whether the mechanical holding areas remain accessible and whether the positioning system interferes with the openings.
A suction cup evaluation would examine whether sufficient solid contact areas are available for the proposed vacuum arrangement.
The correct choice depends on the actual hole distribution, blank dimensions, and bending sequence—not merely on the fact that the product is an electrical cabinet panel.
This distinction is useful for manufacturers working with cabinets, enclosures, ventilation covers, and other sheet metal products containing functional cutouts.
5. Which Technical Specifications Should You Compare Before Buying?
Once both feeding methods have been evaluated, the next step is to confirm machine capacity.
A suitable feeding arrangement cannot compensate for a machine that lacks the required bending size, material capacity, or forming clearance.
According to STON’s published product information, the company offers different press arm and suction cup machine sizes, welded or cast body configurations, CNC servo control, and model-dependent bending capacities.
These specifications vary by model and must not be treated as universal values across the entire product range.
Essential Technical Checklist
| Especificaciones |
Why It Matters |
| Material grade |
Different materials have different forming requirements |
| Minimum and maximum thickness |
Helps identify a suitable machine configuration |
| Flat blank length and width |
Determines machine size and feeding compatibility |
| Finished flange height |
Confirms whether the required forming geometry is possible |
| Return bends and corner details |
Helps identify potential tool interference |
| Minimum forming dimensions |
Determines compatibility with smaller features |
| Bending accuracy |
Establishes finished-part acceptance requirements |
| Surface finish |
Helps define permissible contact and handling conditions |
| Tooling configuration |
Confirms compatibility with the required bending sequence |
| Capacidad de producción |
Supports model selection and workflow planning |
Why should you avoid comparing maximum thickness alone?
A maximum thickness specification is normally defined under particular material and processing conditions.
For example, the capacity for cold-rolled steel should not automatically be applied to stainless steel or aluminum. Machine size, bending length, material properties, and tool configuration can also affect the actual forming limits.
The same principle applies to accuracy and production speed: performance should be confirmed for the workpiece and machine configuration under consideration.
For model-specific information, review the STON CNC Panel Bender technical range and request engineering confirmation for your parts.
6. How Does STON Evaluate Feeding Compatibility Before Machine Selection?
A reliable equipment proposal should begin with an engineering review of the customer’s actual product requirements.
Rather than making a selection based only on whether a customer produces cabinets, furniture, or HVAC equipment, the review should establish how the proposed machine will handle the workpiece during the full bending process.
Recommended Drawing Review Process
Step 1 — Collect Representative Drawings
Provide flat blank drawings and finished-part drawings, including bends, holes, openings, dimensions, and material specifications.
Step 2 — Identify Suitable Holding Areas
Evaluate where the workpiece can be contacted during positioning. For press arm feeding, review mechanical holding accessibility. For suction cup feeding, review suitable vacuum contact areas.
Step 3 — Check Forming Feasibility
Confirm the bending height, return edges, corner geometry, forming clearance, and required bending sequence.
Step 4 — Match the Machine Configuration
Compare the requirements with the appropriate STON model, feeding assembly, tooling plan, and available automation options.
Step 5 — Define Representative Sample Tests
Select parts that can demonstrate actual handling reliability, finished-part accuracy, surface appearance, and production workflow.
This process helps reduce the risk of selecting a machine that performs well during a simple demonstration but is not suitable for the factory’s more demanding production parts.
What Should a Representative Test Verify?
| Test Item |
Required Verification |
| Loading |
Workpiece can be handled reliably |
| Positioning |
Sheet remains correctly located during processing |
| Clearance |
No unacceptable interference with holes or formed features |
| Doblado |
Required sequence can be completed |
| Finished dimensions |
Part meets agreed drawing tolerances |
| Surface condition |
No unacceptable contact marks or scratches |
| Tiempo de ciclo |
Complete production time is measured |
| Operator involvement |
Manual adjustments are identified |
These are recommended validation criteria. Specific sample results should only be published after actual testing.
For context, STON has published overseas panel bending projects, including three CNC panel benders supplied for cabinet and furniture manufacturing in Turkey. That project confirms the general equipment application, but its published information does not identify the individual machines’ feeding configurations or measured cycle times.
7. Which Feeding System Offers Better Production Efficiency?
Neither press arm nor suction cup feeding is automatically faster in every application.
A machine’s published bending movement speed is only one part of the production cycle. Actual output also depends on how efficiently the sheet is loaded, positioned, bent, and unloaded.
For an effective comparison, evaluate:
Total Cycle Time = Loading + Positioning + Bending + Unloading + Required Handling Adjustments
A representative comparison should use the same workpiece drawing, material, acceptance criteria, and production conditions wherever practical.
What Should Buyers Measure?
| Evaluation Item |
Why It Matters |
| Loading time |
Identifies how quickly the blank enters the process |
| Positioning time |
Shows the handling efficiency of each feeding method |
| Complete bending cycle |
Measures the actual finished-part processing time |
| Operator intervention |
Reveals additional adjustments or handling |
| Finished-part quality |
Prevents speed gains from hiding quality problems |
| Product changeover |
Evaluates suitability for different production orders |
For high-volume production, reliable repeated handling can be as important as the bending speed itself.
For a high-mix sheet metal workshop, compatibility across different part designs may offer greater value than achieving a short cycle time on one standard sample.
If your factory intends to introduce robotic loading or a larger automated production layout, feeding compatibility should also be reviewed alongside the material transfer and unloading requirements.
8. What Information Should You Send STON to Get the Right Panel Bender Recommendation?
The fastest way to narrow down the right configuration is to provide sufficient information before requesting a formal quotation.
A basic enquiry containing only the desired machine size and material thickness may not reveal the handling and bending difficulties of the actual part.
| Information to Provide |
Recommended Details |
| Part drawings |
2D and/or 3D files |
| Material |
Grade and surface condition |
| Espesor |
Minimum and maximum production thickness |
| Flat blank dimensions |
Length and width |
| Finished geometry |
Flange height, return bends, and corner details |
| Openings |
Holes, slots, ventilation patterns, and cutouts |
| Surface requirements |
Visible areas, protective films, and finish criteria |
| Volumen de producción |
Expected daily or shift output |
| Product variety |
Number of recurring part designs |
| Current workflow |
Existing cutting, punching, and bending process |
| Necesidades de automatización |
Manual loading, robotic handling, or future integration |
Provide at least one frequently produced part and one difficult part. This gives the engineering team a more realistic understanding of your factory’s requirements.
Final Selection Recommendation
Choose a press arm CNC panel bender when its mechanical positioning arrangement is compatible with your actual workpieces and planned production.
Consider suction cup feeding when a customized vacuum contact arrangement offers a suitable alternative for the part geometry, contact locations, and handling requirements.
For either configuration, verify machine capacity, tooling, forming clearance, finished-part quality, and the complete production cycle before finalizing the purchase.
The best CNC panel bender is the one that can produce your parts reliably—not simply the one with the most attractive catalogue specifications.
Preguntas Frecuentes
Is a press arm CNC panel bender better than a suction cup panel bender?
Neither is universally better. Press arm feeding uses mechanical positioning, while suction cup feeding uses vacuum-based handling. The correct choice depends on the workpiece’s contact areas, geometry, surface condition, and bending requirements.
Which feeding system is better for perforated metal panels?
It depends on the opening distribution and available holding areas. Press arm feeding requires compatible mechanical positioning locations, while suction cup feeding requires suitable vacuum contact areas. Actual drawings and representative tests should determine the choice.
Can a suction cup panel bender handle stainless steel?
Yes, suitable suction cup panel bender configurations can process stainless steel within their specified capabilities. However, the actual material grade, thickness, surface condition, suction contact, and forming requirements must be verified.
Does suction cup feeding prevent surface scratches?
Not automatically. It uses a different contact method, but suction cup condition, material surface, protective films, and handling movements can still influence finished-part appearance. Testing with actual production material is recommended.
Which CNC panel bender is more suitable for electrical cabinet manufacturing?
Both configurations can be evaluated for electrical cabinet production. The selection should be based on cabinet door dimensions, openings, panel structure, material, production volume, and the required handling method.
What does STON need to recommend a CNC panel bender?
Provide material specifications, thickness, flat blank dimensions, finished-part drawings, surface requirements, product variety, target production capacity, and automation requirements. These details support model selection and a representative testing plan.
Conclusion: Choose Around the Workpiece, Not Just the Feeding Technology
Press arm and suction cup CNC panel benders offer different methods of automated sheet positioning and feeding. Their suitability should be evaluated through actual workpiece requirements rather than general assumptions about which technology is better.
Key Takeaways:
- Press arm feeding uses mechanically controlled positioning.
- Suction cup feeding uses vacuum-based holding and can be evaluated with customized suction arrangements.
- Las perforaciones, las formas irregulares, los recubrimientos y las superficies delicadas pueden influir en la compatibilidad con el sistema de alimentación.
- El espesor del material, las dimensiones de la máquina, las herramientas y la geometría de plegado también deben ser compatibles con el modelo seleccionado.
- La revisión de planos representativos y las pruebas con muestras aportan criterios de compra más sólidos que la mera comparación de catálogos.
¿Necesita ayuda para elegir la paneladora CNC adecuada?
STON ofrece soluciones de panelado con brazo de presión y ventosas para distintas necesidades de producción de chapa metálica.
Comparta los planos de sus productos, las especificaciones de los materiales, las dimensiones de los paneles y el volumen de producción previsto. Nuestro equipo de ingeniería puede evaluar la aplicación y recomendar una máquina y una configuración de alimentación adecuadas.
Submit Your Drawings & Request a Custom Solution


 21 de octubre de 2026